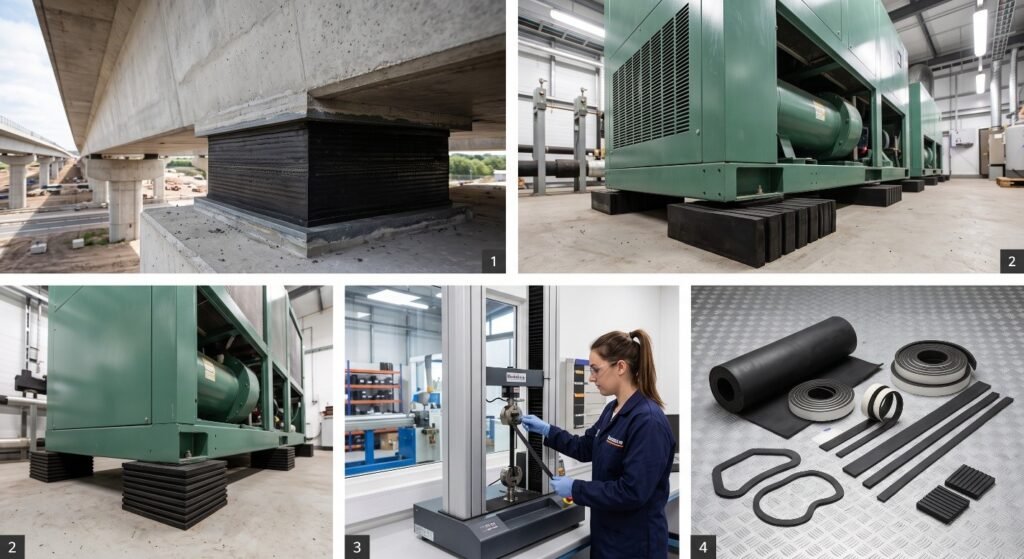
Neoprene (chloroprene) rubber provides exceptional balanced resistance to weathering, physical abrasion, and moderate chemical exposure. However, the success of a Neoprene gasket, lining, or vibration pad depends entirely on the integrity of its installation. Achieving a permanent, waterproof bond requires a strict combination of solvent-based contact cement and uniform clamping pressure.
Surface Preparation and Adhesive Application Contact cement chemically welds the Neoprene to the substrate. Both surfaces must be thoroughly cleaned with a solvent like isopropyl alcohol to remove dust, oils, or mold-release agents left over from the manufacturing process. A uniform layer of contact cement is then brushed or rolled onto both the Neoprene sheet and the mating surface.
The Flash-Off Phase Unlike traditional adhesives, contact cement must not be joined immediately. The coated surfaces require a critical waiting period—typically 5 to 15 minutes—to allow the solvents to fully evaporate. The adhesive should feel tacky but must not transfer to your knuckle when lightly touched. If the pieces are joined while the adhesive is still wet, the solvent becomes permanently trapped, resulting in a weak bond that will fail under shear stress.
Alignment and Clamping Pressure Because contact cement bonds instantly upon touch, there is no margin for repositioning. Once the Neoprene sheet is carefully aligned and placed onto the substrate, immediate pressure is mandatory. Applying mechanical pressure—using C-clamps for rigid substrates, flat presses, or heavy seam rollers—forces out trapped air bubbles and ensures complete surface contact. This uniform pressure is what finalizes the molecular cross-linking, providing a strong, flexible bond that matches the elasticity of the Neoprene itself.
Frequently Asked Questions
Are you currently trying to bond Neoprene to a specific substrate like steel, concrete, or another elastomer?
WhatsApp us